
High Precision Machining Lead Times: What Drives Them, and the Time Budget Precision Carries
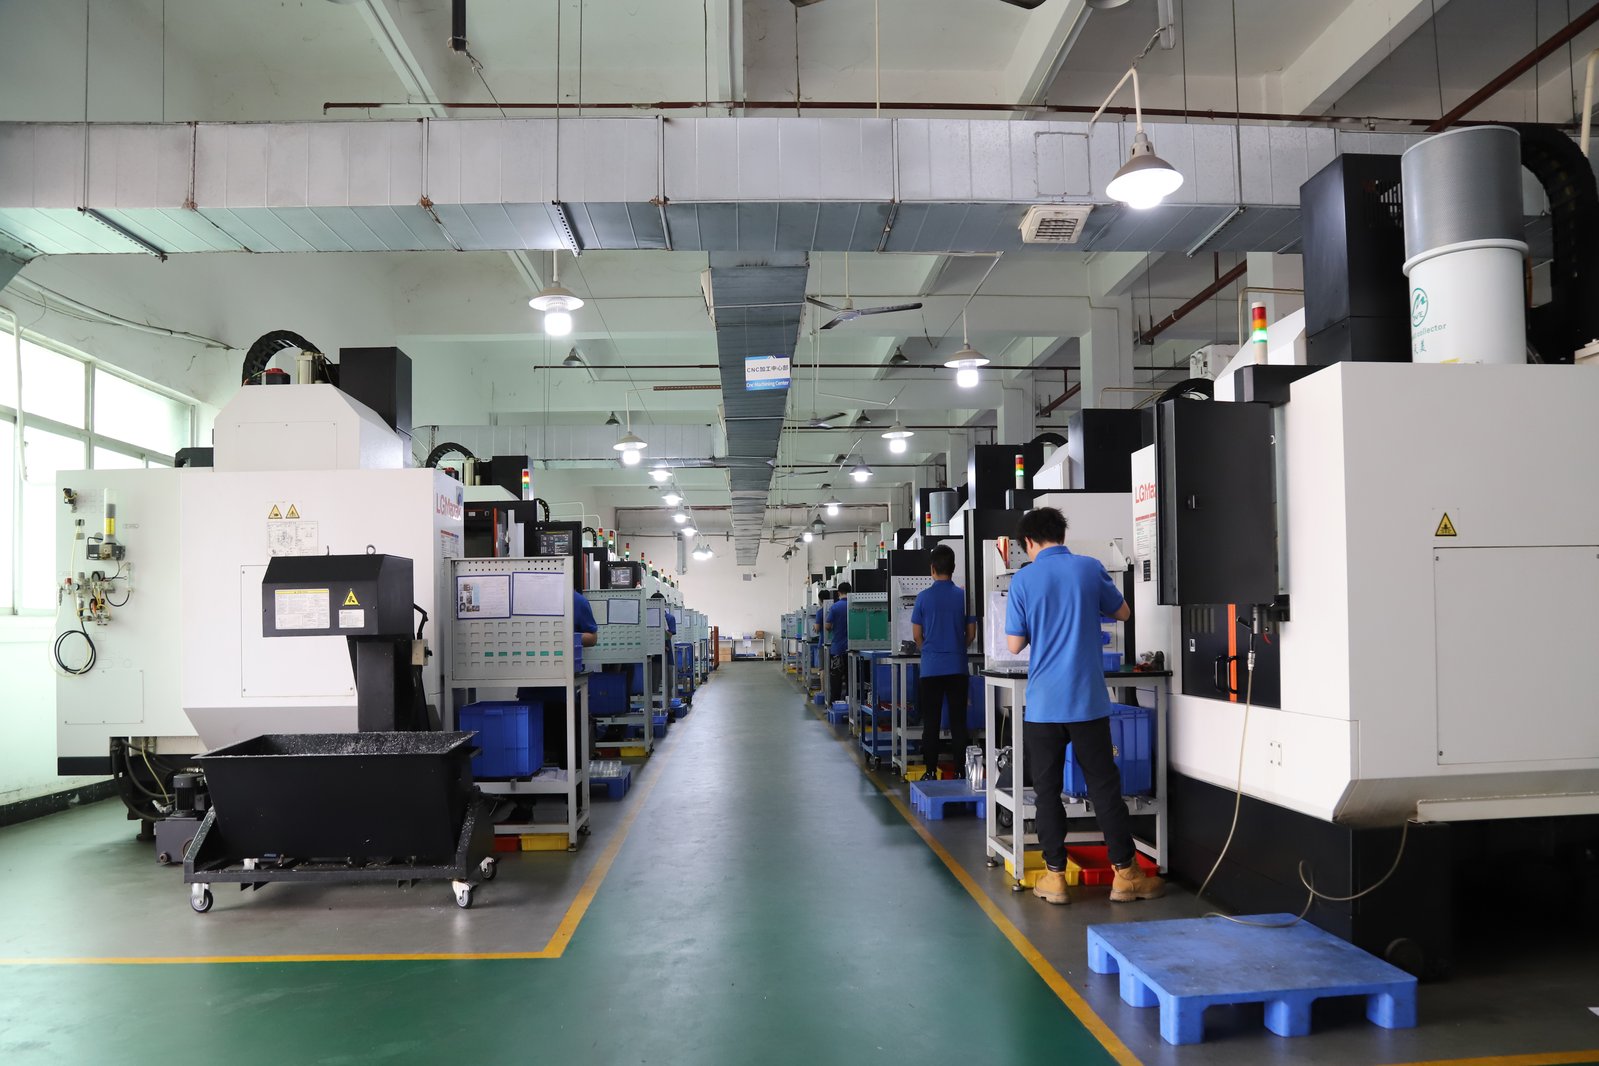
When a quote for a high precision machining order comes back with a delivery date measured in weeks and the drawing contains only minutes of cutting, the obvious conclusion is that the schedule is padded. On a tight-tolerance part, the opposite is usually true. Most of the quoted lead time is not scheduling slack; it is a floor set by the precision itself. Heat has to settle before a micron band can be trusted, and feeds have to drop before a fine surface can be cut. Offsets have to be probed and corrected before the next feature is touched, and the first article has to be released before the rest of the batch is allowed to run. That sequence is physics and procedure, not queue management, and no expediting request removes it. The skill a buyer actually needs is the ability to read a tolerance list as a time budget — to see which slice of a quoted date responds to pressure and which slice the drawing fixes in place.
This guide answers four practical questions. The first two are mechanical: why precision consumes calendar time at the physical level, and how to convert the tolerance callouts on your drawing into a five-segment lead-time budget. The second two are commercial: what a quoted date is really covering, and which actions genuinely shorten the precision-driven portion of the calendar without loosening a single tolerance you need.
Why does a tighter tolerance consume calendar time before the machine even starts?
Temperature and tolerance are the same subject once a band drops below roughly ±0.01 mm. Metals expand and contract with heat, and the numbers are not subtle: a meter of aluminum grows about 24 µm per degree Celsius, steel about 12 µm, titanium about 9 µm. A ±0.003 mm callout — ten microns wide in total — can be crossed by a couple of degrees of temperature difference on a part that is only a few hundred millimeters long. That is why the reference temperature of 20 °C sits behind standard dimensional metrology, and why critical dimensions on this floor are measured on CMMs rather than at the bench. It is also why a thick-walled part that leaves a warm roughing operation cannot be finish-cut and measured on faith. The part has to come to thermal equilibrium with the machine and the metrology room first. On a heavy forging or a large plate that wait is measured in hours, and it is serial: it happens once per temperature-sensitive operation, not once per batch in parallel.
Precision also sets the pace of the cutting itself. The finishing pass that lands a fine surface or holds a tight bore is taken slowly, with light engagement and a small depth of cut, because material removal rate is exactly what you give up to protect the surface and hold the dimension. Roughing can be aggressive; the precision finish pass cannot. A feature that needs multiple finishing passes, or a re-cut after an offset correction, consumes wall-clock time that does not scale with quantity the way a standard operation does.
Then come the judgment loops that standard-tolerance work never enters. A tight feature earns an in-machine measurement, a comparison against the intended value, a correction, and often a re-cut, and an operator or a probing routine makes that decision serially, feature by feature. A drawing with two or three functionally critical bores at ±0.003 mm carries several of these loops; a drawing that pins twenty features to the same tight band carries twenty, whether the function needs any of them. The loops are sequential and they occupy the machine; none of that time shows up in a simple "hours of machining" estimate.
Finally, the first article gates the batch. On a high-precision part you do not run 200 pieces and then check one; the first piece is inspected against the drawing, the process is confirmed, and only then does the run continue. The first-article release is a scheduling hard point on this class of work. It is why the calendar around a new precision drawing always contains a visible pause between "program ready" and "batch running." A supplier that treats that gate as a formality is describing work it does not actually do.
How do you convert a tolerance list into a lead-time budget?
A quoted lead time is not one number; it is five segments stacked end to end, and each segment obeys different rules. Once you can name the segments, a delivery date stops being a black box and becomes a budget you can sanity-check against the drawing.
| Segment of the lead time | What sets its length | Does expediting help? |
|---|---|---|
| 1. Queue and quoting | Shop loading, capacity at the moment your PO lands, engineering review time | Yes — this is the only segment that is genuinely about scheduling |
| 2. Standard machining | Quantity, material, number of operations | Partly — more machines can split a run, within reason |
| 3. Precision adder | How many features carry tight bands and how tight they are; grows as tolerances tighten | No — serial loops of cut, measure, correct cannot be parallelized |
| 4. Inspection and first-article release | CMM capacity, thermal conditioning before measurement, documentation | Indirectly — earlier process qualification shortens the release gate |
| 5. Transport | Your freight lane and customs, not the factory | Only by paying for faster freight |
Read the table against your own drawing and the picture changes immediately. If the part carries a general tolerance block with one or two tight features, segment 3 is small and the date is mostly queue plus standard machining plus shipping — compressible in the normal ways. If the drawing blankets every dimension at ±0.003 mm, segment 3 grows disproportionately, because every tight callout adds serial loops that no second machine can absorb. The single most useful estimate a buyer can make before requesting a quote is how many features genuinely need the tight band, because that count is what drives the precision adder.
The precision adder is also where the tolerance type matters, not just the number. A ±0.003 mm diameter on a turned feature may require a finish pass, a probe check, and possibly one compensation cut. A tight true-position callout on a bore pattern forces a datum alignment, repeated probing across features, and a final CMM verification of the whole pattern as a group — a longer serial sequence than any single size tolerance. Roundness or cylindricity on a running journal does the same. When you convert a drawing to a time budget, the features that consume the adder are not the ones with the most decimal places on paper. They are the ones whose tolerance can only be confirmed by measurement against a datum or a form — exactly the work that cannot be rushed. Which of those claims survive your own gauges and which ones need a CMM report is covered separately in the tolerance verification guide on this site.
What is a quoted date actually covering, and what does it assume about your process?
Every precision shop quotes its delivery date inside an assumed process, and the assumption is rarely written down. A 20-something-day quote for a tight-tolerance order quietly assumes a thermal soak for temperature-sensitive material, cutter paths validated for the finish passes, a first-piece release gate, and a CMM slot long enough for the part to reach measurement temperature. When you read a date, the productive question is not "is that the fastest you can go" but "which of these assumptions is true for my part on the first run."
The difference between suppliers on precision work shows up exactly here. One operating model qualifies the process before the batch: it cuts and measures trial pieces, validates the program and the inspection routine, and confirms the first article early enough that the documented release is ready before the production run is scheduled. On repeat orders of a qualified part, the precision adder mostly disappears from the calendar because the process is already proven. The other model qualifies on the batch itself. Here the first article is inspected only when production reaches it, and the CMM report is generated as part of the run. Any drawing ambiguity or process gap is then discovered in the middle of the calendar rather than before it. Both shops can quote the same tolerance. The second one eats the same serial loops inside your delivery date; the first one has already spent that time before you placed the order.
For a buyer, that is why the tolerance conversation belongs in the quotation stage, not the delivery stage. Ask what the date assumes. Is first-article release included in the quoted lead time, or separate from it? Is the CMM report for the tight features produced on the batch, or on a trial part cut earlier? And do repeat orders of the same drawing run on the already-qualified process? The answers tell you which of the five segments is actually inside the number you are being quoted. The drawing side of this conversation — what the term "high precision" must mean on your quote so the tolerance and the date are both honest — is the subject of the site guide to precision machining on drawings, quotes, and inspection reports.
How do you shorten the precision-driven part of the calendar without loosening a tolerance you need?
Expediting pressure moves segment 1 and almost nothing else. To move the precision adder, you have to change when work happens, not how hard someone pushes. The actions below are the ones that actually work, and all of them happen before the PO or in the first days after it.
- Run the trial cut during the quotation period, not after the PO. Ask the supplier to cut and verify a sample or a representative feature while the quote is being prepared. If the program and inspection routine are validated and the first article is released before the order is placed, the batch starts from an already-qualified process, and the precision adder shrinks to the production features themselves.
- Send the inspection requirement with the drawing. State which features need a CMM report, the reference temperature, and the acceptance criteria before quoting begins. A supplier who can schedule the CMM work and the release gate up front will quote a tighter date than one who discovers the paperwork when the parts are done.
- Grade your tolerances before you send the file. Tighten only the two or three features that control function — the bores that locate, the seat that seals, the journal that runs — and leave the rest on a standard band. Each feature moved from the tight band to the general block removes a serial measurement-and-correction loop from segment 3. This is the same right-tight discipline that keeps precision cost under control, and it compresses time the same way it compresses price.
- Parallelize only what is genuinely parallel. If a drawing contains an unproven precision feature next to a long run of standard work, a second supplier or a split of the standard operations can overlap the runs. What cannot be parallelized is the serial qualification of the tight feature itself, so spend the parallel capacity on the standard volume, not on pretending the precision loop can be shared.
- Write the lead-time structure into the PO. Ask for the date in three pieces: first-article release date, batch completion date, and ship date. A supplier that can name the release gate is managing the precision segment; one that offers only a single ship date is asking you to trust the arithmetic.
Notice what is absent from this list: asking the shop to skip the first-article inspection, to measure at the bench instead of on the CMM, or to run the batch before the tight feature is confirmed. Those shortcuts do not compress the precision adder; they move risk from the calendar onto your line. A dimensional report that ships with every batch, with key characteristics charted to Ppk ≥ 1.67 initial, is part of the process described on this site's quality control page. It is also the reason the date can be trusted once it is given.
The mental shift is small and the payoff is large: stop treating a high-precision lead time as a scheduling promise and start treating it as a physics statement with a budget you helped design. If the drawing is graded, the trial cut is done early, and the inspection gate is agreed before the PO, most of the precision adder is already spent — before your order ever lands in the queue.
Frequently Asked Questions
Why can't a ±0.003 mm feature simply be expedited?
Because the tight band is confirmed through serial work — thermal settling, slow finish passes, probe checks, offset corrections — and that sequence cannot be shortened by scheduling pressure or additional machines. Expediting moves the queue ahead of you; it does not compress the precision adder that the tolerance itself creates.
Which part of a precision lead time can actually be compressed?
The queue segment responds to expediting, and standard machining can be split across machines within reason. The precision adder and the first-article gate compress only by doing work earlier: qualifying the trial cut during quoting, grading tolerances down to the features that need them, and agreeing the inspection plan before the PO.
Does every tight dimension add the same amount of time?
No. A single tight diameter may need one finish pass and one probe check, while a tight position callout on a bore pattern forces datum alignment and group verification on the CMM — a longer serial sequence. Features whose tolerance is only provable against a datum or a form cost the most calendar time, because that measurement work cannot be rushed.
Why does first-article release sit in the middle of the calendar rather than at the end?
On precision work the first piece is inspected and the process confirmed before the batch is allowed to run, because you do not discover a process gap after 200 parts exist. The release gate therefore divides the schedule into "qualify" and "produce," and suppliers who validate the trial part before the PO effectively move that gate into the quotation period.
How much inspection time does a tight tolerance add to a batch?
The inspection itself is a fraction of the calendar; the constraint is the CMM slot and the thermal conditioning that precedes a trustworthy reading. Parts must sit at measurement temperature before critical dimensions are verified, so tight features add both machine time and waiting time — another reason the precision adder grows as tolerances tighten.
Does a single precision prototype take as long as a production batch to release?
The first-article release is what takes the time; running additional parts afterward is comparatively fast. A single prototype therefore earns most of the precision adder, which is why a trial part ordered during the quotation period is such a cheap way to compress the eventual production date.
What should a lead-time quote state about tolerances before it counts as a commitment?
The date should state whether first-article release is included or separate, which tight features will be verified on the CMM and at what reference temperature, and whether repeat orders of the same drawing run on the already-qualified process. A quote that names the release gate is a commitment; one that names only a ship date is a hope.
When should I send the drawing if the tolerances are tight and the launch date is fixed?
Earlier than you think, and with the tolerance grades and inspection requirements already marked. The precision adder is front-loaded: the trial cut, the release gate, and the CMM verification all happen before the batch runs. Sending an ungraded drawing two weeks before launch does not leave the supplier two weeks — it leaves them a first-article release to complete inside those two weeks.
Working toward a fixed launch date with tight tolerances on the drawing?
Send your file and target date to [email protected] or call +86 13126536955, and the team will map the tolerance list against the calendar before you commit — naming the features that set the pace, whether a trial cut in the quoting period can reclaim weeks, and what a realistic first-article release looks like for your part.